Why a horizontal vibrating screen needs synchronized exciters
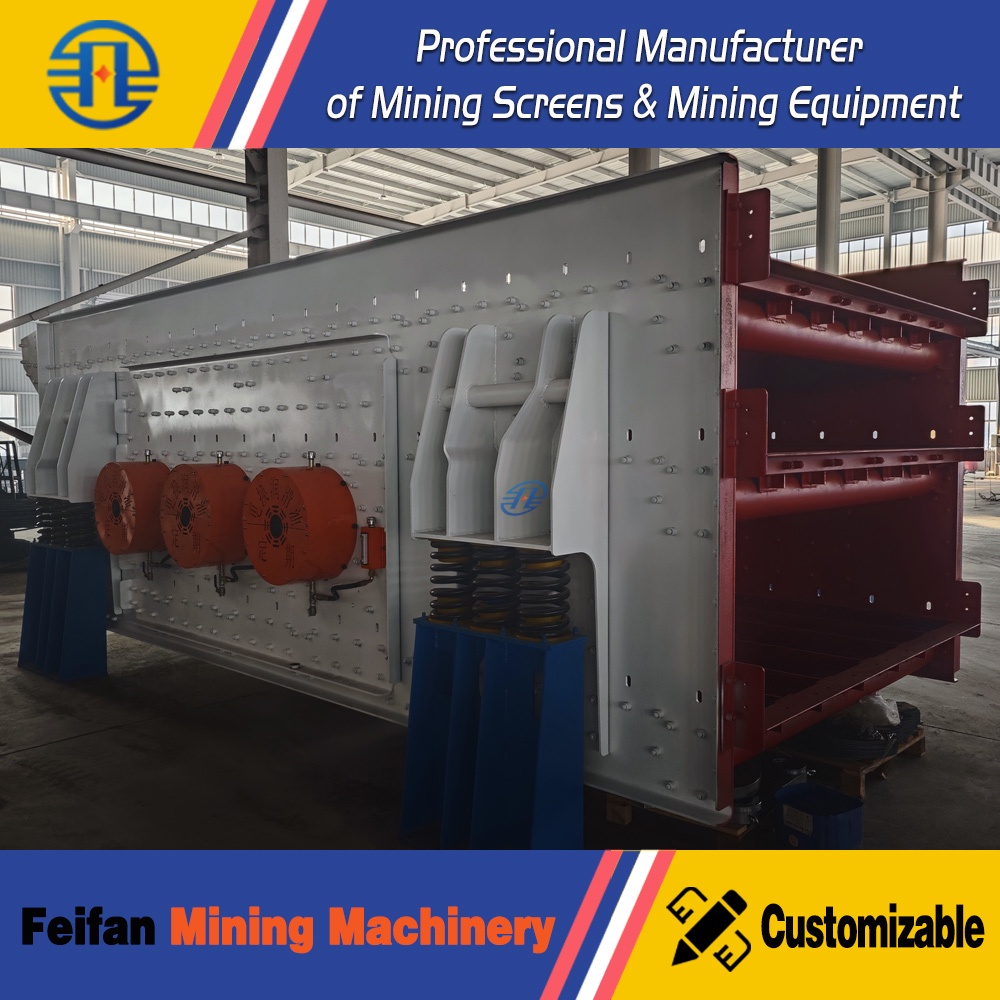
A horizontal vibrating screen needs synchronized exciters because their combined forces determine the direction and consistency of the deck’s motion. With little or no deck slope to move material forward, the screen relies on a controlled throwing action to convey aggregates while allowing smaller particles to pass through the openings. Exciters running at the correct speed but with the wrong phase relationship can produce an unsuitable throw direction, uneven movement, or changing loads on the screen structure.
Synchronization means maintaining the designed relationship between rotating eccentric masses. It does not necessarily mean that every shaft turns in the same direction or that every counterweight occupies the same angular position. The required relationship follows the screen’s exciter arrangement and intended motion.
The deck needs a directed throw
On an inclined screen, gravity contributes substantially to material travel. A horizontal deck depends more heavily on its vibration trajectory: the combination of vertical lift and horizontal movement that advances the material bed. During each cycle, particles lose contact with the surface, move through a short flight, and land farther along the deck.
The vertical component helps loosen the bed, allowing smaller particles to work downward toward the screening surface. The horizontal component provides transport. Their balance affects bed depth, residence time, and the opportunities particles have to encounter an opening.
A throw directed too steeply can produce vigorous bouncing with insufficient forward travel. A throw directed too shallowly can reduce bed loosening. Increasing excitation force without correcting the trajectory does not necessarily improve screening; it can increase motion while leaving the underlying transport problem unresolved.
How synchronized eccentric masses create the intended motion
Each rotating eccentric mass generates a centrifugal force whose direction changes continuously. In a common two-shaft linear arrangement, equal eccentric masses rotate in opposite directions at the same speed. Their timing makes selected force components cancel while the components along the intended throw line reinforce one another.
The resulting excitation acts back and forth along that line. Its angle relative to the deck establishes the relationship between lift and forward movement. The screen box responds to this excitation through its mass, stiffness, suspension, and material load.
Matching shaft speed alone is insufficient. Two shafts can rotate at the same speed while maintaining an incorrect angular relationship. That phase offset changes how their forces combine. In an ideal equal-force, counter-rotating pair, a steady phase offset can rotate the resultant force line rather than automatically producing an elliptical path. A phase relationship that keeps changing makes the excitation direction unstable.
Unequal eccentric forces introduce another distinction. Even with stable timing, mismatched counterweights or incorrect weight settings prevent complete cancellation of the intended opposing components. The resultant excitation can then become elliptical. This is why phase, rotational direction, speed, and eccentric moment must be considered together.
Some horizontal screens deliberately use elliptical motion, including arrangements with additional synchronized shafts. An elliptical trajectory is therefore not inherently a fault. The meaningful comparison is between measured motion and the trajectory specified for that particular machine.
What keeps the exciters synchronized?
Mechanical synchronization uses gears, connecting shafts, or another positive timing arrangement to maintain the required relationship. Correct assembly establishes the phase. Gear timing, coupling condition, and the specified counterweight positions remain relevant after bearing work, exciter replacement, or drive repairs.
Other designs use self-synchronizing drives. Separate exciters interact through the vibrating structure and settle into a stable operating relationship under suitable design and loading conditions. Simply powering two motors at the same frequency does not establish that their eccentric masses are correctly phased. Electrical frequency controls motor speed characteristics; synchronization also involves the mechanical response of the complete screen.
Electronically coordinated systems are another possibility, but their control requirements depend on the equipment design. A speed reference without angular feedback should not be assumed to provide direct phase control.
These arrangements have different service requirements. A gear-coupled exciter needs its mechanical timing preserved during assembly. A self-synchronizing system needs the specified rotation directions, compatible exciter settings, and suitable structural and suspension conditions to establish stable motion.
Screening performance reveals the consequences
Disturbed excitation often first appears as a change in material movement. Material can accumulate near the feed end, travel unevenly across the width, or discharge at an inconsistent rate. A deeper bed gives fine particles farther to travel before reaching the mesh, while rapid passage reduces the time available for separation.
These symptoms do not identify synchronization trouble by themselves. Wet feed, excess throughput, blocked apertures, and uneven feed distribution can produce similar results. A useful distinction is whether the screen box’s measured trajectory has changed along with material behavior.
For example, poorer separation with a stable, specified trajectory points attention toward feed conditions, screen media, or loading. Poorer separation accompanied by a shifting throw angle, abnormal transverse movement, or different motion on opposite sides requires investigation of the excitation system and the structure supporting it.
Wear patterns add context. Concentrated wear along one side can reflect uneven feed loading, damaged media supports, or torsional movement. It is evidence to compare with motion measurements, rather than proof of incorrect exciter timing.
Why bearings and the screen structure are affected
The screen box is designed around a particular pattern of cyclic forces. When the resultant excitation changes direction or becomes unevenly distributed, side plates, crossmembers, exciter mountings, and connections experience a different loading pattern. Additional twisting or transverse motion can increase local fatigue loading even when the machine’s overall stroke appears familiar.
Bearing temperature and noise also require interpretation. Lubrication problems, contamination, incorrect fits, and bearing damage can produce similar symptoms. Abnormal excitation changes bearing loading, but a hot bearing alone does not establish a synchronization fault.
Startup and shutdown deserve separate attention. Passing through structural resonances can temporarily produce larger movements than steady operation. Persistent beating, repeated impacts, or motion that fails to settle after reaching operating speed calls for investigation. The acceptable transient behavior must come from the machine’s design information, rather than a universal vibration limit.
Measurements that separate timing faults from other problems
A useful assessment combines operating speed, shaft phase where measurable, and motion at several locations on the screen box. A single amplitude reading cannot describe the complete vibration pattern.
- Compare corresponding points on both sides. Differences in stroke or trajectory can reveal twisting, uneven loading, or structural problems that a measurement near one exciter misses.
- Record the feed and discharge ends as well. Some variation follows the machine’s design, but a new difference under comparable conditions needs explanation.
- Confirm what the instrument reports: peak amplitude and peak-to-peak displacement are different quantities. Comparing them directly creates a false discrepancy.
- Where the design permits phase measurement, use shaft reference signals or the specified diagnostic method. Matching speed readings alone cannot confirm correct timing.
Measurements under no-load and representative loaded conditions help distinguish a persistent mechanical issue from a load-sensitive response. Feed rate, moisture, and material distribution should be recorded with those readings so that unlike operating conditions are not treated as equivalent.
After exciter maintenance, restoration of the specified timing, rotation directions, and eccentric settings should precede performance adjustments. Increasing counterweight settings to recover throughput can conceal an incorrect trajectory while increasing dynamic forces. Any physical inspection or timing adjustment requires isolation of the drive and control of stored mechanical energy.
The useful acceptance criterion is a stable trajectory consistent with the screen’s design across its intended operating conditions. Exciter synchronization establishes the force relationship that makes that motion possible; measurements of the assembled, loaded machine show whether it is being achieved.
Leave A Message
If you are interested in our products and want to know more details, please leave a message here, we will reply you as soon as we can.